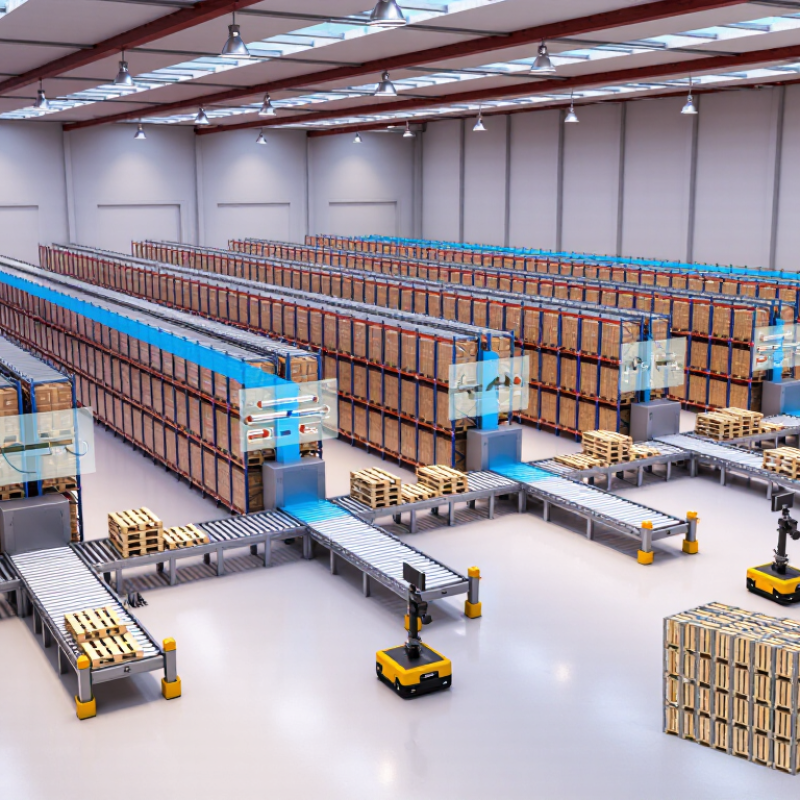
| System Definition | Pallet flow racking is a dynamic storage system that uses inclined roller or wheel lanes to move pallets by gravity from the loading side to the picking side. | Creates controlled pallet movement without requiring a forklift to enter every storage lane. | Confirm that the pallet base, load weight, and pallet condition are compatible with the lane equipment. |
| Inventory Rotation | FIFO — First In, First Out | Each lane normally has loading access at one end and unloading access at the opposite end, supporting stock rotation. | Best suited to products with expiration dates, batch controls, or a need for chronological inventory movement. |
| Alternative Operating Mode | LIFO — Last In, First Out | Single-sided flow lanes can be used when the newest pallet should be retrieved first or when stock rotation is less critical. | Use only when product shelf life and inventory-control procedures permit non-FIFO operation. |
| Primary Movement Principle | Gravity-driven movement on a slight incline, with brakes, speed controllers, or separators used to regulate pallet travel. | Reduces horizontal travel and can improve throughput in high-volume pallet storage areas. | Roller resistance, pallet quality, lane length, load distribution, and temperature can affect movement. |
| Typical Lane Incline | Approximately 3%–5%, subject to pallet type, load weight, roller design, and supplier engineering. | Provides enough gravitational force for controlled pallet movement while limiting excessive speed. | The final slope must be calculated and tested for the actual pallet and load combination. |
| Typical Storage Depth | Commonly about 2–20 pallet positions per lane; deeper configurations are possible with specialized engineering. | Allows multiple pallets of the same product or batch to be stored in one lane. | Greater depth improves density but may reduce selectivity and increase requirements for load control. |
| Pallet Access | Direct forklift access is generally provided at the loading and unloading faces rather than throughout the lane. | Supports high-density storage while reducing the number of aisles required compared with conventional selective racking. | Plan forklift turning space, approach clearances, rack-end protection, and pedestrian separation. |
| Load Capacity | Capacity is project-specific and commonly ranges from several hundred kilograms to more than 1,000 kg per pallet position. | Allows the system to serve light, medium, and heavy palletized goods when correctly engineered. | Never select capacity from a generic range; verify beam, frame, roller, pallet, and floor-load calculations. |
| Pallet Compatibility | Compatible pallets must have adequate bottom boards, runners, or support surfaces to pass over the rollers or wheels. | Ensures stable travel, correct braking, and safe transfer through the lane. | Check pallet dimensions, bottom-board spacing, deflection, damage rate, and material type before installation. |
| Common Rack Components | Frames, beams, roller lanes, guide rails, lane dividers, speed controllers, pallet stops, separators, and back protection. | Components work together to support the load and control pallet movement. | Component selection should match lane depth, pallet mass, operating speed, and forklift handling method. |
| Storage Density | High density compared with selective pallet racking, because fewer operating aisles are required. | Maximizes warehouse cube utilization for products stored in multiple pallets per stock-keeping unit. | High density may reduce SKU selectivity; use a product velocity and inventory-profile analysis before choosing the layout. |
| Best-Fit Product Profile | Large quantities of similar products, limited SKU variety per lane, and goods requiring regular pallet replenishment. | Works well in food and beverage, cold storage, wholesale distribution, manufacturing, and high-volume logistics operations. | Consider selective or shuttle systems when the warehouse requires very high SKU variety or frequent individual pallet access. |
| Temperature Suitability | Can be designed for ambient, chilled, and frozen environments when materials, lubricants, clearances, and corrosion protection are suitable. | Supports controlled-temperature storage and helps organize temperature-sensitive inventory. | Specify operating temperature, condensation exposure, corrosion risk, and cleaning requirements during design. |
| Throughput Factors | Throughput depends on pallet arrival rate, lane depth, forklift travel, loading method, unloading method, and product mix. | Separating loading and unloading faces can reduce traffic conflicts and support continuous replenishment. | Use real order, replenishment, and dispatch data instead of relying only on nominal rack capacity. |
| Safety Equipment | Typical safety provisions include pallet stops, speed control, guide rails, upright guards, back stops, warning signs, and load notices. | Controls pallet movement and helps protect the rack, operators, forklifts, and stored goods. | Safety features must be selected according to the local code, risk assessment, rack configuration, and operating procedures. |
| Inspection and Maintenance | Regular inspections should check frames, beams, connectors, rollers, brakes, pallet stops, guards, labels, and visible damage. | Maintains performance and helps identify defects before they cause pallet instability or rack failure. | Inspection frequency should reflect site risk, usage intensity, damage history, and applicable local requirements. |
| Relevant Design References | Common references include local building regulations, warehouse-racking design rules, and recognized guidance such as EN 15629, EN 15635, or applicable ANSI/RMI requirements. | Provides a framework for specification, installation, inspection, and safe use. | The governing standard depends on the installation country, project scope, and authority having jurisdiction. |
| Manufacturer Evaluation Criteria | Engineering capability, tested components, load calculations, pallet-flow expertise, installation quality, spare-parts support, and inspection services. | Helps buyers compare worldwide suppliers without relying only on price or advertised capacity. | Request project references, structural calculations, technical drawings, warranty terms, testing evidence, and after-sales support details. |
| Main Advantages | High storage density, controlled stock rotation, reduced aisle requirements, organized replenishment, and good use of warehouse height. | Can improve space utilization and operational consistency in suitable product environments. | Benefits are highest when pallet standards, SKU grouping, and loading discipline are consistent. |
| Main Limitations | Lower selectivity than selective racking, dependence on pallet quality, more complex lane components, and higher design sensitivity. | Highlights situations where another storage technology may provide better flexibility or lower total cost. | Compare pallet flow with drive-in, carton flow, selective, push-back, or automated shuttle solutions using total-cost analysis. |